A smooth, narrow laser weld can look impressive, but surface appearance does not reveal how deeply the metals have fused. In industrial fabrication, inadequate penetration can leave an apparently finished joint vulnerable to separation, while excessive penetration may cause burn-through, porosity, or distortion.
Understanding laser weld penetration is therefore essential when selecting welding equipment and developing reliable production parameters. Manufacturers such as Dynalasers offer handheld laser welding systems with different power levels and material-specific rated depths, but actual performance depends on more than machine wattage.
What Is Laser Weld Penetration?
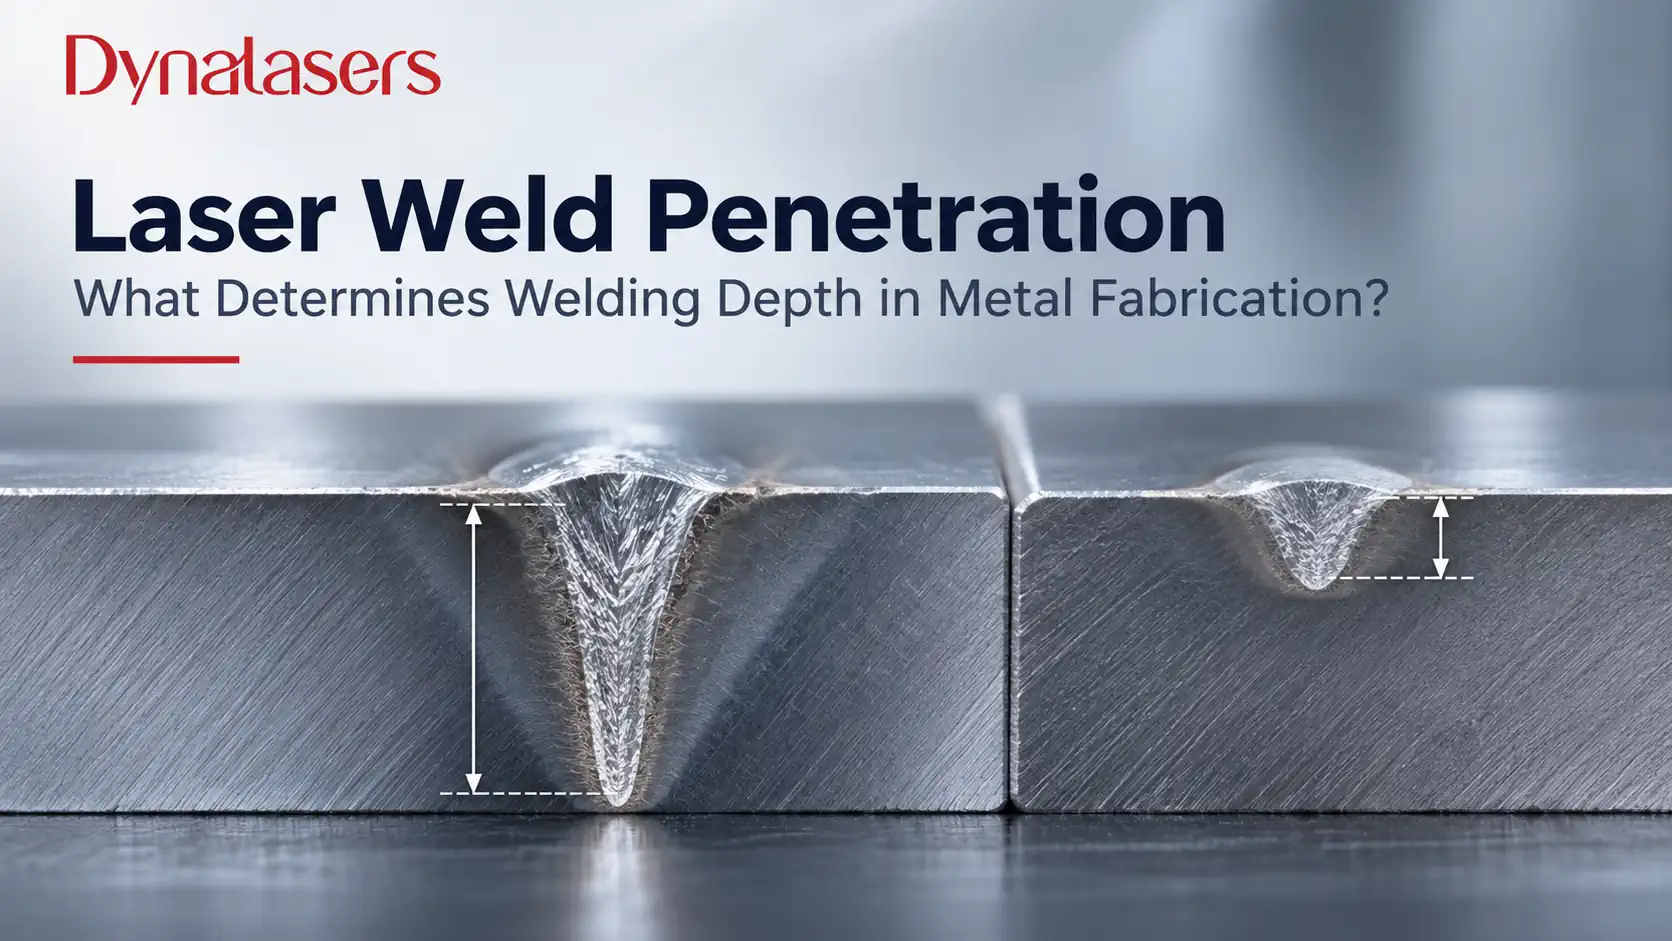
Laser welding penetration depth describes how far the fusion zone extends into the workpiece from a defined reference surface. Unlike weld bead width, which describes the visible or measured lateral dimensions, penetration represents the depth of material melted and resolidified during welding.
Three measurements help engineers understand the resulting joint:
- Penetration Depth: The distance from the specified reference surface to the deepest point of fusion.
- Weld Width: The lateral dimension of the fused region at a defined location.
- Fusion Zone: The material that melted and resolidified, forming the metallurgical joint.
A narrow laser welding bead may contain substantial internal fusion, while a visually smooth, relatively wide bead can still have inadequate penetration.
This is particularly important for lap joints, where the laser must reach and fuse the interface between overlapping sheets. For butt joints, the requirement may instead involve full-thickness penetration or a specified partial-penetration weld.
Penetration should always be evaluated against the intended joint geometry, not simply the visible surface profile.
Conduction vs. Keyhole Laser Welding: Why Penetration Differs
The depth of a laser weld depends partly on how energy enters the material. Two important operating modes are conduction welding and keyhole laser welding.
Conduction welding transfers heat primarily from the workpiece surface into the surrounding metal. At higher power densities, vaporization can form a narrow cavity known as a weld keyhole, allowing laser energy to reach deeper regions.
| Factor | Conduction Welding | Keyhole Welding |
|---|---|---|
| Energy Transfer | Mainly heat conduction | Vapor cavity and multiple internal reflections |
| Weld Geometry | Relatively shallow and wide | Relatively deep and narrow |
| Typical Application | Thin components and shallow joints | Deeper fusion and thicker joints |
| Main Concern | Insufficient penetration | Keyhole instability, porosity, or spatter |
Industrial deep penetration welding can operate at power densities around 1 MW/cm². Under suitable conditions, penetration depth may reach approximately ten times the weld width, with some industrial systems achieving depths up to 25 mm.
These are general industrial process capabilities, not typical performance guarantees for portable handheld welders.
In deep penetration laser welding, metal vapor pressure maintains the cavity while molten metal flows around it and solidifies behind the moving beam.
However, an unstable keyhole can collapse and trap gas, creating internal pores. Achieving maximum possible depth is therefore less important than maintaining stable fusion without defects.
What Factors Affect Laser Weld Penetration?
Actual penetration results from the interaction of laser power, travel speed, beam focus, material properties, and joint preparation. In fiber laser welding, changing one parameter can influence several aspects of the molten pool simultaneously.
| Welding Parameter | Effect on Penetration | Potential Problem |
|---|---|---|
| Laser Power | Higher available energy may increase fusion depth | Burn-through, spatter, unstable keyhole |
| Travel Speed | Changes energy delivered per unit length | Shallow fusion or overheating |
| Focal Position | Influences spot size and power density | Reduced or inconsistent penetration |
| Material Properties | Absorption and thermal conductivity affect melting | Different depths at identical settings |
| Beam Oscillation | Redistributes energy across the weld | Excessive width or reduced depth |
| Filler Wire | Changes deposited material and joint filling | Poor fusion if feeding and beam settings are mismatched |
A useful starting calculation is nominal laser energy per unit weld length:
Linear Energy (J/mm) = Laser Power (W) ÷ Travel Speed (mm/s)
For example:
- Laser output: 1,200 W
- Travel speed: 20 mm/s
- Nominal linear energy: 60 J/mm
Reducing the travel speed to 15 mm/s increases nominal linear energy to 80 J/mm, a 33% increase.
However, this does not mean penetration increases by 33%. The calculation does not account for optical absorption, focal position, beam oscillation, thermal losses, or keyhole stability.
The same principle applies to laser welding with filler wire. Additional wire may improve gap filling and weld geometry, but depositing more metal does not automatically increase fusion into the base material.
For production engineers, the objective is to establish a stable parameter window rather than maximizing any individual setting.
How Deep Can Dynalasers Handheld Laser Welders Penetrate?
Buyers often ask how deep laser welding penetrates before selecting equipment. The answer depends on material type, joint geometry, and the machine’s available power and processing configuration.
Dynalasers offers S, M, and D Series handheld laser welding systems covering different fabrication requirements. Their published capabilities provide useful equipment-selection references, but they should not replace representative weld testing.
Dynalasers S Series: Thin-Sheet and Localized Welding
Image Name: s-series-portable-handheld-laser-welder-dynalasers
Image Alt: Dynalasers S Series Portable Handheld Laser Welding Machine
The Dynalasers S Series includes S10 Spot, S30, and S40, with compact configurations for thin metal parts, localized welding, and portable fabrication.
| Model | Published Welding Capability | Key Feature |
|---|---|---|
| S10 Spot | Single-sided welding below 1 mm | Compact design, under 10 kg |
| S30 | Approximately 2.5 mm maximum depth | Continuous, burst, and pulse modes |
| S40 | Application-dependent | Compact handheld configuration |
The S10 Spot’s published thin-sheet capability applies to compatible stainless steel, carbon steel, and galvanized steel. For thin components, excessive penetration and burn-through can be as problematic as insufficient fusion.
Dynalasers M Series: Power and Material Penetration
Image Name: m-series-handheld-laser-welder-dynalasers
Image Alt: Dynalasers M Series Handheld Fiber Laser Welder
The Dynalasers M Series covers multiple power configurations, including the M71 five-in-one energy-storage welding system.
| Model | Rated Power | Published Stainless Steel Capability |
|---|---|---|
| M30 | 800W | Up to 3 mm penetration |
| M50 | 1200W | Up to 5 mm penetration |
| M70 | 1800W | Up to 7 mm penetration |
| M71 | 1800W | Up to 3+3 mm lap welding |
Material differences are significant even with the same equipment. For example, the M70 has the following maximum manufacturer-rated penetration figures:
| Material | M70 Maximum Rated Penetration |
|---|---|
| Stainless Steel | 7 mm |
| Carbon Steel | 7 mm |
| Aluminum | 5.5 mm |
| Brass | 6 mm |
| Copper | 2.5 mm |
These differences reflect the importance of material absorption, thermal conductivity, and process conditions. They should not be interpreted as guaranteed production depths for every joint.
The M71 adds dual-wobble technology, seven scanning patterns, and single- or dual-wire feeding. These features provide more configuration options for different joints, although their effects on penetration must be tested individually.
Dynalasers D Series: Integrated Air-Cooled Welding
Image Name: d-series-industrial-laser-welder-dynalasers
Image Alt: Dynalasers D Series Industrial Handheld Laser Welder
The Dynalasers D Series offers integrated air-cooled equipment for workshops requiring different welding power levels.
| Model | Rated Power | Maximum Rated SS Penetration |
|---|---|---|
| D50P | 1200W | 5 mm |
| D70P | 1800W | 7 mm |
The D50P weighs under 41 kg, while the D70P weighs under 43 kg.
Their integrated configurations can simplify equipment placement, but an integrated design does not inherently produce deeper welds than other systems of comparable processing capability.
How to Achieve Consistent Penetration Without Welding Defects
A successful demonstration weld is not enough to establish reliable production conditions. Actual laser weld penetration must remain consistent despite changes in operator technique, material batches, surface preparation, and component fit-up.
A practical development procedure involves:
- Use representative joints. Test actual production materials, thicknesses, joint gaps, and fixtures.
- Establish a controlled parameter window. Adjust one variable at a time while documenting power, speed, focus, and oscillation settings.
- Inspect the optical system. Contaminated protective windows or changes in beam delivery can reduce effective energy at the joint.
- Measure weld cross-sections. Verify fusion depth and boundaries using appropriate cutting, polishing, etching, and microscopy procedures.
- Check repeatability. Examine several welds produced under normal operating conditions rather than relying on one favorable result.
Cross-sectional inspection introduces another practical challenge: the fusion boundaries of narrow laser welds may be harder to reveal than those of conventional arc welds.
A poorly polished sample, inappropriate etchant, or inadequate magnification can obscure the boundary. If the fusion zone is unclear, the preparation and examination procedure should be reviewed rather than assuming that penetration is absent.
More importantly, increasing laser power is not always the correct solution. Excessive energy can produce unstable keyholes, internal porosity, excessive root penetration, or burn-through.
The best welding parameters are those that repeatedly achieve the required fusion geometry while keeping defects within the applicable acceptance criteria.
Frequently Asked Questions
Is Full Penetration Always Necessary in Laser Welding?
No. Full penetration is required for certain joints, but partial-penetration welds can be acceptable when their effective weld size and mechanical performance satisfy the design requirements. The correct target depends on joint geometry, loading conditions, and applicable specifications.
Can Multiple Laser Welding Passes Increase Joint Fusion?
Additional passes may increase the total fused region or complete a joint that cannot be welded in one pass. However, multiple passes introduce additional thermal cycles and potential defects. Their combined effect must be evaluated through a qualified welding procedure rather than assuming that individual penetration depths simply add together.
Why Can Laser Weld Penetration Decrease During Extended Operation?
Possible causes include optical contamination, changes in focal position, unstable output, material variation, and altered travel speed. Engineers should compare current operating data against a validated baseline and inspect equipment condition before changing the welding schedule.
Conclusion
Reliable laser weld penetration depends on energy concentration, material properties, joint preparation, and stable processing parameters. A visually attractive bead or maximum rated welding depth cannot independently establish production quality.
With compact S Series machines, flexible M Series options, and integrated D Series systems, Dynalasers offers several welding configurations for different fabrication requirements. Representative sample testing remains the most reliable way to match equipment capability with actual penetration needs.